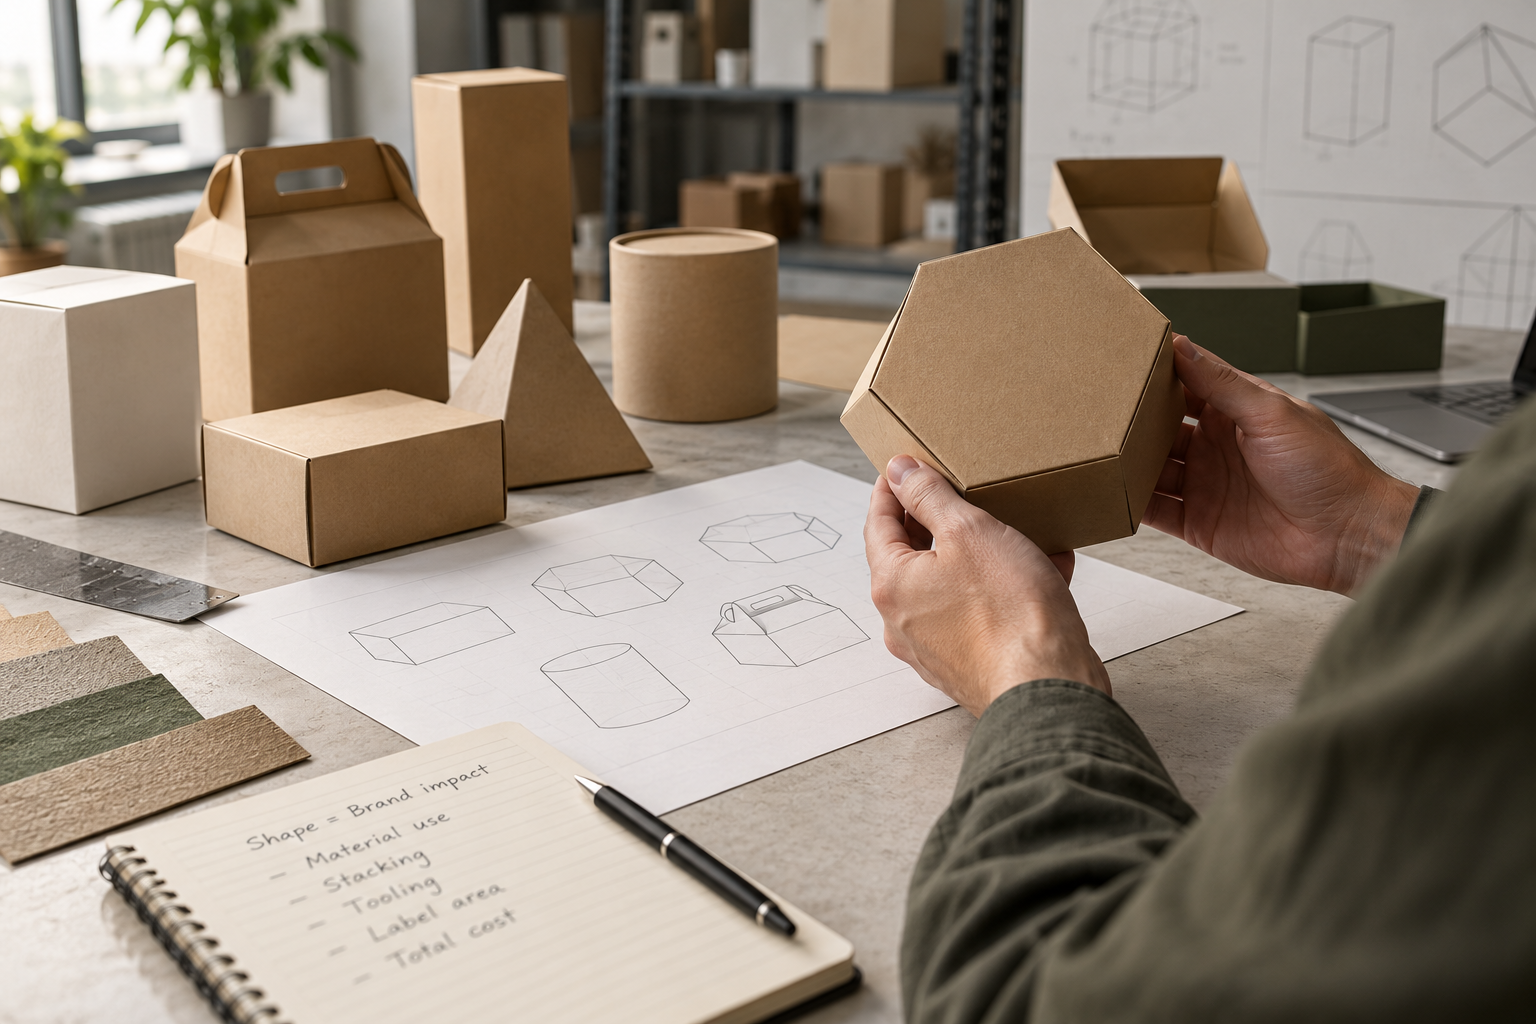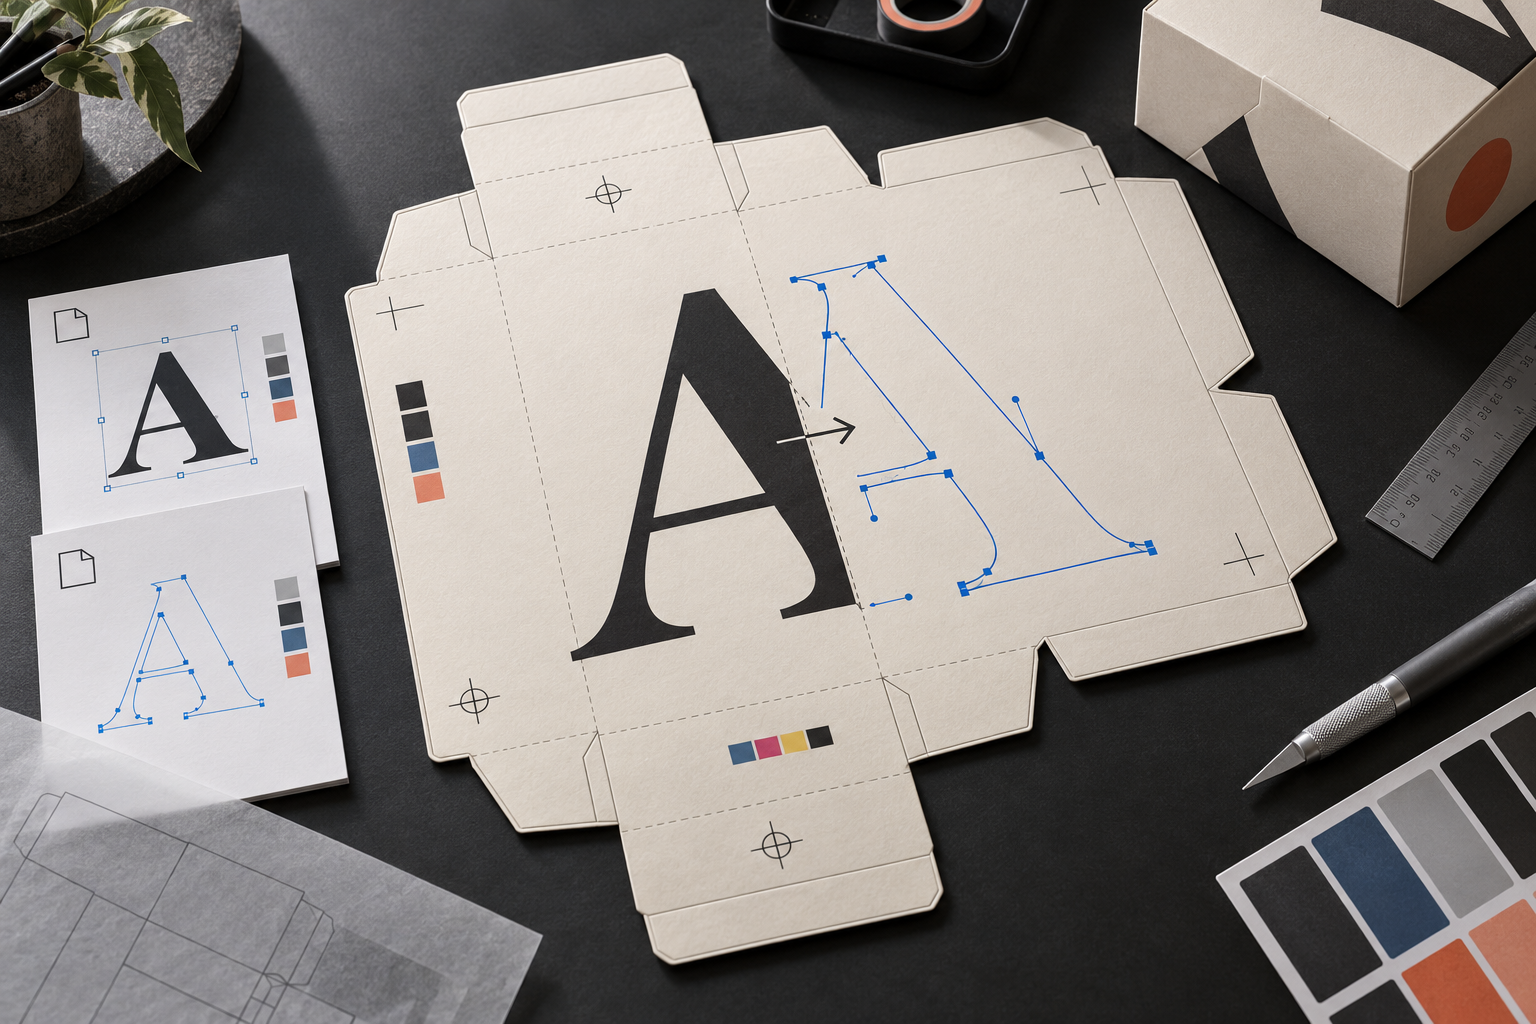
Making product packaging is not the same as placing artwork on a box. A package must contain and protect the product, run on the packing line, communicate required information, scan correctly, survive its distribution route, work for the consumer, and reach an acceptable total cost.
Those priorities can conflict. In Ryder's March 2026 survey of 1,160 U.S. online shoppers, among respondents who preferred receiving orders in boxes, 32% cited perceived transit protection, 29% reuse, and 20% environmental friendliness. These are self-reported perceptions from an e-commerce survey—not proof that a box is the best format for every product—but they illustrate how users judge several packaging functions at once. Ryder study announcement; Packaging Dive analysis.
The reliable way to make packaging for a product is therefore a gated development process: define the system, convert needs into measurable requirements, engineer and cost the solution, validate the complete packaged product, and control what enters production.
First, define the complete packaging system
A product rarely has only one package. Using precise package levels prevents a team from solving the retail presentation while overlooking distribution.
Table 1. The package levels to define before design begins.
Package level | Typical role | Examples | Questions to answer |
|---|---|---|---|
Primary package | Directly contains or contacts the product | Bottle, jar, tube, pouch, can, tray, sachet | Is it compatible with the product and filling process? Does it provide the required barrier, seal, dispensing, and shelf life? |
Secondary or presentation package | Groups, protects, or presents one or more primary packs | Folding carton, sleeve, multipack, display-ready tray | Is it required for protection, labeling space, tamper evidence, bundling, or shelf presentation? |
Shipping case | Protects sellable units during warehousing and transport | Corrugated regular slotted case, wraparound case | How many sellable units fit, how are voids controlled, and can the case withstand the defined route and stacking conditions? |
Unit load | Moves multiple shipping cases through the supply chain | Pallet, slip sheet, stretch-wrapped load | Are footprint, height, weight, stability, warehouse handling, and retailer requirements defined? |
E-commerce shipment configuration | Reaches the consumer through a parcel network | Product package shipped alone, mailer, overbox with cushioning | Will the item ship in its own packaging or receive additional fulfillment packaging? What route-specific test or retailer certification applies? |
“Outer box” is too imprecise for a technical specification. Use secondary package, shipping case, or overbox according to the actual function.
The 10-step product packaging development process
Each stage should end with a deliverable and an approval decision. Skipping a gate often moves the problem downstream, where changing tools, printed inventory, or launch dates becomes more expensive.
Table 2. A practical stage-gate workflow.
Step | Work to complete | Required deliverable | Approval gate | Typical owner |
|---|---|---|---|---|
1 | Define the product, user, sales channels, distribution route, forecast, launch date, and target economics. | Packaging brief | Business and channel assumptions approved | Brand / product |
2 | Map the primary pack, presentation pack, shipping case, pallet, and e-commerce configurations. | Packaging-system map | No package level or handoff is missing | Packaging / operations |
3 | Translate product and route risks into measurable requirements. | User requirement specification | Requirements, methods, and acceptance criteria agreed | Packaging / quality |
4 | Develop structural concepts and select candidate materials and processes. | Concept drawings, preliminary bill of materials, risk review | Preferred concept chosen for evidence—not appearance alone | Packaging engineering |
5 | Establish category rules, label copy, claims, warnings, symbols, and required data. | Regulatory and claims matrix | Product-category reviewer clears the content plan | Regulatory / legal |
6 | Build the dieline, artwork, print specification, coding zones, barcode, and version control. | Controlled artwork package | Copy, dimensions, separations, and identifiers approved | Brand / prepress |
7 | Source suppliers and compare total delivered cost, capacity, tolerances, quality systems, and continuity. | Comparable quotations and supplier assessment | Commercial and technical source approved | Procurement / quality |
8 | Produce prototypes, samples, tooling trials, and pilot packs on representative equipment. | Prototype and pilot report | Manufacturability and pack-out risks acceptable | Supplier / operations |
9 | Validate compatibility, shelf life, usability, line performance, distribution, and channel requirements. | Approved validation report | Predeclared acceptance criteria met | Quality / engineering |
10 | Release the specification, approved sample, inspection plan, and change-control process. | Production specification and control plan | Only controlled versions may be ordered and produced | Quality / operations |
This workflow can be compressed for a low-risk line extension, but the team should record which assumptions were reused and why. “Same material” or “same box” does not prove that a new product, closure, fill weight, route, or artwork will perform identically.
Step 1–3: turn the product brief into measurable requirements
Do not start by asking whether the package should be paper, plastic, glass, or metal. Start with what the packaged product must do.
Table 3. Inputs that should become packaging requirements.
Input | Examples to record | Packaging decision affected | Evidence to request |
|---|---|---|---|
Product properties | Liquid, powder, oil, acid, fragrance, alcohol, light sensitivity, oxygen or moisture sensitivity | Material compatibility, barrier, sealant, closure, headspace | Formulation data, compatibility plan, migration or interaction assessment as applicable |
Filling and processing | Fill temperature, pressure, speed, sterilization, freezing, cooling, coding | Material grade, dimensional tolerance, seal window, line equipment | Line specification and pilot-trial protocol |
Shelf-life target | Required duration, temperature, humidity, light, opening and reclosing | Barrier, closure, coating, desiccant, secondary protection | Shelf-life protocol with product and package measurements |
Consumer use | Opening force, dispensing, portion control, grip, resealing, storage, instructions | Closure, ergonomics, tamper evidence, copy hierarchy | Use test with the intended user and realistic product |
Distribution route | Parcel, LTL, full truckload, mixed pallet, export, cold chain, number of handling stages | Shipping case, cushioning, unit load, test sequence | Route map, carrier or retailer requirements, approved test plan |
Retail and digital shelf | Shelf dimensions, peg/display method, facings, theft risk, mobile thumbnail, returns | Geometry, presentation panel, identifiers, image system | Retailer specifications and actual-size shelf/digital review |
Quality risk | Leakage, breakage, scuffing, crushed corners, unreadable codes, contamination | Critical-to-quality features and inspection plan | Defect definitions, sampling plan, measurement method, limits |
Volume and operations | Forecast, SKU count, variants, order frequency, storage, manual or automated packing | Tooling, process, MOQ, inventory, changeovers | Demand scenario, capacity and lead-time confirmation |
A requirement must be testable. “Premium,” “durable,” and “sustainable” are directions, not specifications. Replace them with observable conditions: approved color tolerance, maximum leak rate, compression criterion, target opening experience, verified recycled-content percentage, or defined source-reduction comparison.
Step 4: select structure and material as one system
Material cannot be selected independently of format and manufacturing. A folding carton, corrugated shipping case, rigid bottle, flexible pouch, thermoformed tray, and molded-fiber insert use different converting methods, tolerances, decoration options, tooling, filling systems, and recovery pathways.
Compare concepts against the same weighted criteria:
Criterion | Questions for concept selection |
|---|---|
Product protection | Does the design control leakage, breakage, contamination, barrier loss, and product movement? |
Manufacturing | Can the supplier hold the dimensions and properties required by the filling and packing process? |
Distribution | Does the complete loaded package suit the actual parcel, case, pallet, temperature, and handling route? |
Consumer use | Can the intended consumer open, dispense, reclose, store, and dispose of it as intended? |
Communication | Is there sufficient usable area for required labeling, instructions, coding, barcode placement, and brand hierarchy? |
Economics | What is the total delivered and operating cost, not only the component price? |
End of use | Is the claim supported by the complete construction, collection access, sorting, processing, and relevant market rules? |
Supply resilience | Are tooling ownership, backup material, alternate site, lead time, and change-notification terms clear? |
A lower material price can create a higher system cost if it slows the line, increases damage, requires an overbox, creates obsolete inventory, or causes chargebacks.
Step 5–6: reserve compliance, barcode, and production space before artwork
Regulatory requirements depend on the product, claim, package, and jurisdiction. The examples below are selected U.S. checks, not a universal label checklist.
Table 4. Selected U.S. packaging and labeling controls.
Area | Current reference point | Development implication |
|---|---|---|
Food-contact materials | FDA states that food packaging components—including relevant adhesives and colorants—may be food-contact substances. The authorization must fit the substance, manufacturer where applicable, food type, and conditions of intended use. FDA food-contact overview | Validate the complete food-contact construction and intended use; a generic supplier statement that a material is “FDA approved” is not enough. |
Packaged-food information panel | Under 21 CFR §101.2, covered information must generally be prominent and conspicuous, with letters or numbers no smaller than 1/16 inch, unless an applicable exception is established. | Measure usable panels and required copy before finalizing package dimensions. The figure is not a universal minimum for every declaration or category. |
General consumer commodities | 16 CFR Part 500 addresses identity, manufacturer/packer/distributor information, and net quantity for consumer commodities within its scope, while listing category exclusions governed elsewhere. | Identify the responsible regulator before applying a label template. Do not copy food, cosmetic, or household-product rules across categories. |
Child-resistant packaging | The CPSC's Poison Prevention Packaging Act guidance states that certain household substances require packaging significantly difficult for children under five to open while remaining usable by normal adults. | Determine whether the product is covered and complete the applicable special-packaging testing and certification process. |
Environmental marketing | The FTC Green Guides advise against broad unqualified “green” claims and explain substantiation and qualification for recyclable, recycled-content, compostable, refillable, and source-reduction claims. | Build claim substantiation alongside the package; do not add environmental language after material selection without reviewing the full construction and market access. |
Product identification | GS1 lists the General Specifications version 26.0.0 as current from January 27, 2026. GS1 US notes that placement, size, quiet zones, print surface, and proportional scaling affect scan performance. | Allocate a suitable barcode zone on the structural drawing and verify the printed symbol, rather than checking only the digital artwork. GS1 US placement guidance |
Artwork should be built on the released structural dieline, not the other way around. Keep required text, barcode quiet zones, date/lot coding, seams, folds, glue areas, closures, and retailer labels out of conflict. Define color targets, substrates, finishes, trapping, overprint, screening, proof type, print process, and version in the controlled artwork specification.
Step 7: compare total packaging cost, not the unit quote
Use the same cost boundary for every concept and supplier. A practical planning model is:
Total delivered packaging cost per sellable unit
= purchased components + printing/conversion + tooling amortization + packing labor or co-pack fees + expected scrap + inbound freight + storage and inventory carrying cost + applicable program fees + expected packaging-related damage and returns
This is a management framework, not a required accounting formula. Finance should define the company's treatment of tooling, overhead, inventory, and failure cost.
Table 5. Data required for a comparable supplier quotation.
Data group | Fields to request or confirm |
|---|---|
Exact specification | Material and grade, dimensions and tolerances, caliper or thickness, construction, coatings, inks, adhesives, finish, closure, count and packing method |
Commercial basis | Price breaks, MOQ, economic order quantity, setup, plates/cylinders, tooling, proofs, testing, freight basis, taxes/duties where applicable, payment terms |
Operations | Normal and expedited lead time, run rate, changeover, expected yield, overrun/underrun allowance, pallet pattern, storage requirement |
Quality | Critical-to-quality characteristics, sampling plan, defect limits, certificates, lot traceability, retained samples, complaint and corrective-action process |
Supply risk | Tool ownership and location, raw-material lead time, approved alternates, backup site, capacity reservation, disaster recovery, notification before any change |
Sustainability and claims | Component weights, recycled-content evidence, chain-of-custody or other certification scope, recovery claim evidence, state EPR data category where applicable |
Never compare one supplier's ex-works component price with another supplier's delivered, printed, inspected, and packed price without normalizing the scope.
Step 8–9: prototype the package, then validate the complete packaged product
A white sample can confirm size and opening sequence. It cannot prove production print, seal integrity, shelf life, line speed, or distribution performance. Build evidence in layers.
Table 6. Packaging validation matrix.
Validation area | Test unit | What to establish | Typical trigger for retest |
|---|---|---|---|
Product–package compatibility | Intended product in production-representative contact materials | No unacceptable interaction, migration, absorption, corrosion, distortion, odor, or seal effect under intended use | Formula, material, coating, adhesive, colorant, process, temperature, or supplier change |
Seal, closure, and leak performance | Filled pack with intended closure and application settings | Seal/torque/application window and leakage acceptance under defined conditions | Closure, liner, neck finish, fill, capper, sealing equipment, or setting change |
Shelf life and barrier | Filled production-representative pack | Product and package remain within predeclared limits for the intended period and storage conditions | Barrier layer, thickness, closure, headspace, process, or distribution-temperature change |
Packing-line trial | Production-representative components on intended equipment | Run rate, jams, feeds, sealing, coding, scrap, changeover, and inspection capability are acceptable | Dimension/tolerance, substrate, finish, equipment, speed, or supplier-site change |
Distribution performance | Complete loaded package in its shipping configuration | The packaged product meets approved post-test criteria after a route-relevant sequence | Product weight, case count, cushioning, case grade, pallet pattern, carrier, or route change |
Barcode and code verification | Printed production sample | Symbols and variable codes scan and remain legible in expected conditions | Artwork, size, substrate, ink, varnish, print process, coding equipment, or location change |
Consumer use | Filled package with intended users | Opening, dispensing, reclosing, instructions, accessibility, and disposal behavior meet the brief | Closure, geometry, instructions, material stiffness, or target-user change |
For distribution testing, select the method from the route and purpose. ASTM D4169-23e1 provides a sequenced framework for evaluating shipping units against anticipated distribution hazards and states that it does not replace material specifications or existing preshipment procedures. ISTA Procedure 3A addresses individual packaged products moving through parcel systems at 150 lb or less. Neither source creates a universal pass criterion for every CPG package; the team must predefine the test unit, sequence, severity, sample condition, inspection, and acceptance criteria.
Retailer programs may add another layer. Amazon's U.S. Ships in Product Packaging page says eligible FBA products must be grouped by relevant packaging characteristics and a product from each group tested; it currently permits self-testing for qualifying products under 50 lb that do not contain liquids or sharp items, while other products may require an ISTA 6 lab test. This is a retailer program requirement, not a general U.S. packaging rule, and the current guideline must be checked for the specific product at the time of certification.
Step 10: release a specification that another team can reproduce
The approved package is not the sample sitting on a desk. It is the controlled information that allows a supplier, plant, co-packer, inspector, and replacement employee to reproduce the result.
Table 7. Minimum contents of a production packaging specification.
Section | Controlled information |
|---|---|
Identification | Part number, description, SKU use, revision, effective date, owner, approved supplier and site |
Construction | Drawing, dimensions, tolerances, materials, grades, thickness/caliper, coatings, adhesives, inks, closure, finish |
Graphics | Released artwork, color standard, print process, proof reference, copy version, barcode and coding zones |
Packing | Component orientation, units per bundle/case/pallet, protective packing, labeling, storage and handling |
Quality | Critical characteristics, measurement method, sampling, defect classification, acceptance limits, certificate and traceability requirements |
References | Approved sample, validation reports, regulatory/claims approvals, food-contact documentation where applicable |
Change control | Changes requiring notification, approval, new samples, revalidation, new artwork, or inventory disposition |
Retain an approved production sample or agreed objective color/measurement standard where appropriate. Define who can approve deviations and what happens to old inventory after a revision.
What this means for CPG leaders
Packaging development works best as a cross-functional operating process, not a handoff from brand to a supplier.
Name one accountable packaging owner. Brand, regulatory, engineering, procurement, quality, operations, and e-commerce still own their decisions, but one person must control the complete system and timeline.
Approve requirements before appearance. Lock product, route, channel, user, and measurable performance needs before selecting a structure or commissioning final artwork.
Use total cost and risk to choose a concept. Include line performance, freight, inventory, fees, damage, and returns—not only price per component.
Test the package actually being sold and shipped. Use production-representative materials, filled product, closures, shipping case, pallet or parcel configuration, and predefined acceptance criteria.
Release data, not tribal knowledge. A controlled specification, artwork file, approved evidence, inspection plan, and change process are the real production handoff.
Frequently asked questions
Do I need custom packaging for a new product?
Not always. A stock container or standard shipping case can reduce tooling, MOQ, and lead time if it meets the product, line, channel, labeling, and user requirements. Custom structure is justified when a standard format cannot meet the required performance or creates a worse total cost.
Should I design the logo and artwork before the packaging structure?
Develop the brand system early, but finalize artwork only after the structure, usable panels, seams, closures, coding, barcode area, and required copy are defined. Structural changes can otherwise invalidate the layout.
How many prototypes are required?
There is no universal number. The sample plan should reflect product variability, package variability, failure consequence, test method, and decision confidence. A single passing sample provides weak evidence about repeatability.
Is a drop test enough to approve packaging?
Usually not. A drop test addresses only selected impacts. The route may also create vibration, compression, temperature, humidity, leakage, abrasion, pallet instability, and repeated-handling risks. Use a route-relevant test plan and inspect both package and product against predeclared criteria.